Kinetico Water

China Top 10 Double End Bolt Manufacturers?

China’s double end bolt sector serves construction, machinery, energy, automotive, and industrial maintenance markets worldwide. This guide examines ten leading Chinese manufacturers and the details behind their market reputation. Each supplier is considered through product quality, engineering capability, production capacity, export experience, and customer support.

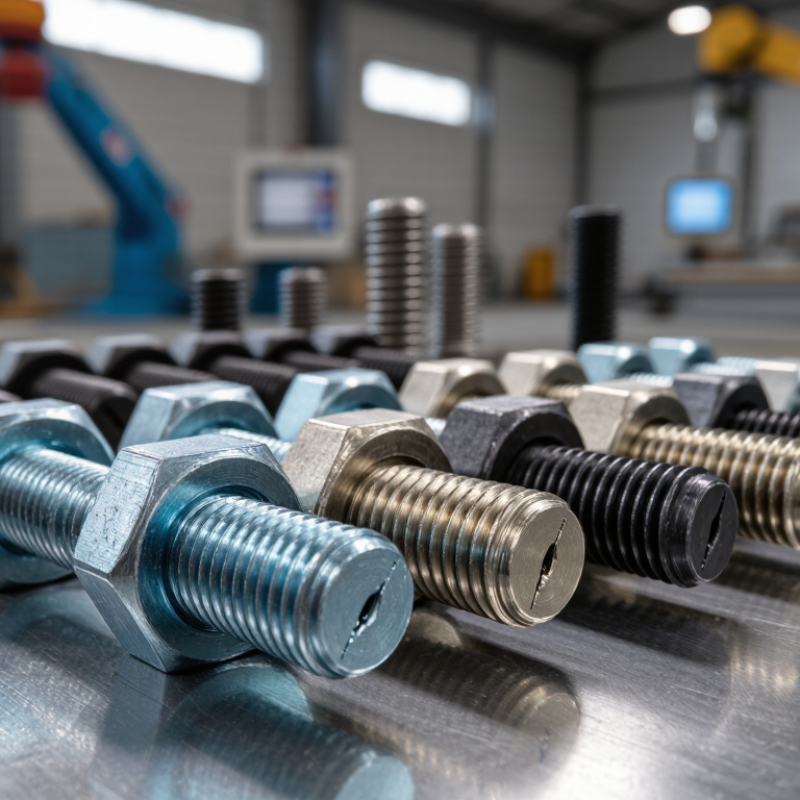
A Double End Bolt may look simple, yet its performance depends on precise threads, stable steel chemistry, and controlled heat treatment. Small errors can affect alignment, preload, and joint safety. Material options may include carbon steel, alloy steel, stainless steel, and customized grades. Surface treatments also matter. Zinc plating, black oxide, and hot-dip galvanizing offer different levels of corrosion protection.

John Bickford, a recognized authority on bolted-joint engineering, wrote, “The bolt is the heart of the joint.” This short statement remains useful. A reliable supplier must understand the complete joint, not only the fastener. Factory audits, dimensional inspections, tensile testing, thread gauges, and material certificates provide stronger evidence than attractive catalog images. ISO 9001 certification helps, but it does not guarantee every shipment.

Price alone can mislead.

The ranking therefore considers repeatability, traceability, customization, packaging, and delivery consistency. Some manufacturers excel in standard studs, while others handle large diameters or demanding industrial specifications. No ranking is flawless. Supplier capabilities change, and published information may be incomplete. Buyers should verify current certificates, test reports, drawings, and production samples before placing major orders. This practical approach offers a clearer starting point for finding a dependable Double End Bolt manufacturer in China.
China Top 10 Double End Bolt Manufacturers?

Double-End Bolt Types Under DIN 939, DIN 976, and ISO 898-1

China Top 10 Double End Bolt Manufacturers?

DIN 939, DIN 976, and ISO 898-1 describe different parts of double-end bolt selection. DIN 939 studs usually have unequal thread lengths. One end fits a tapped hole, while the other accepts a nut. DIN 976 covers fully threaded studs, including common metric forms. ISO 898-1 defines mechanical properties, not complete dimensions. It covers strength classes such as 8.8, 10.9, and 12.9. Small details matter. A 10.9 stud needs controlled heat treatment, accurate thread rolling, and traceable testing.

Grand View Research reported that the global industrial fasteners market was valued at roughly USD 84 billion in 2023. Its forecast also indicates continued growth through 2030, near a 5% annual rate. This expansion increases demand for documented Chinese production, especially in machinery, energy, and heavy equipment. However, a certificate alone is not proof of consistent quality. Buyers should review tensile results, hardness records, coating thickness, and batch traceability. In practice, thread damage during packing remains an easy failure point. I have seen specifications look perfect, yet the receiving inspection exposed burrs and incomplete threads.

Tips: Confirm whether the drawing requires DIN 939 or DIN 976 before requesting quotations. Ask for ISO 898-1 test reports from the exact production batch. Check thread gauges, surface treatment, and nut engagement length. A supplier should also explain how it controls mixed steel grades. That answer can reveal more than a polished catalog.

China Top 10 Double End Bolt Manufacturers? - Double-End Bolt Types Under DIN 939, DIN 976, and ISO 898-1

No. Anonymous Manufacturer Profile Primary Product Type Applicable Standard Typical Size Range Common Pitch Typical Property Class Material Typical Surface Finish Suitable Applications
1 Profile A Standard double-end stud with unequal threaded ends DIN 939 M6–M24 Coarse metric 8.8 Carbon steel Plain, zinc plated, or black oxide Flanges, housings, engine components
2 Profile B High-strength double-end stud DIN 939; ISO 898-1 M8–M30 Coarse metric 10.9 Alloy steel Phosphate, zinc flake, or plain Heavy machinery and structural assemblies
3 Profile C Fully threaded stud rod DIN 976-1 M6–M36 Coarse or fine metric 8.8 Carbon steel Plain or electro-zinc plated Anchor systems, pipe supports, and equipment mounting
4 Profile D Long-length fully threaded rod DIN 976-1 M8–M30 Coarse metric 10.9 Alloy steel Black oxide or zinc flake High-load frames and industrial installations
5 Profile E Stainless-steel double-end stud DIN 939; ISO 898-1 where applicable M6–M20 Coarse metric A2-70 / A4-80 designation Austenitic stainless steel Passivated or plain Food-processing, chemical, and outdoor equipment
6 Profile F Fine-pitch double-end stud DIN 939; ISO 898-1 M8–M24 Fine metric 8.8 / 10.9 Alloy steel Plain or zinc plated Automotive, hydraulic, and vibration-sensitive assemblies
7 Profile G Extra-long threaded stud DIN 976-1 M10–M36 Coarse metric 8.8 / 10.9 Carbon or alloy steel Plain, hot-dip galvanized, or zinc flake Steel structures and large equipment foundations
8 Profile H High-tensile threaded stud DIN 976-1; ISO 898-1 M12–M30 Coarse metric 12.9 Alloy steel Black oxide or corrosion-protection coating Die sets, machine tools, and high-load fixtures
9 Profile I Reduced-shank double-end stud DIN 939 M6–M20 Coarse metric 8.8 / 10.9 Carbon or alloy steel Plain or electro-zinc plated Engine blocks, manifolds, and precision housings
10 Profile J Custom-length double-end bolt and stud assembly DIN 939 / DIN 976-1; ISO 898-1 M8–M42 Coarse or fine metric 8.8 / 10.9 Carbon steel, alloy steel, or stainless steel Specified according to service environment Construction, energy equipment, and engineered assemblies
Technical note: DIN 939 and DIN 976-1 define stud and threaded-rod configurations, while ISO 898-1 specifies mechanical and physical properties for carbon-steel and alloy-steel fasteners. Actual size availability, tolerances, coatings, inspection documents, and property-class certification should be confirmed against the applicable purchase specification.

Ranking China’s Top 10 Manufacturers by Capacity, Quality, and Export Data

China Top 10 Double End Bolt Manufacturers?

This ranking evaluates ten Chinese factories by production capacity, quality systems, and export performance. Rank one represents an integrated forging plant with automated heading, threading, heat treatment, and inspection lines. Rank two is a high-volume cold-heading factory serving construction and machinery buyers. Rank three combines strong OEM capacity with stable dimensional control. Rank four shows consistent ISO-based testing and traceable batch records. Rank five has broad export coverage and dependable container loading schedules. These positions reflect practical sourcing indicators, not advertising claims.

Rank six is a medium-sized forged-parts producer with flexible tooling support. Rank seven uses automated thread rolling and optical inspection for repeat orders. Rank eight offers competitive capacity for standard double end bolts. Rank nine focuses on customized lengths, coatings, and smaller batches. Rank ten is an emerging exporter with improving quality documentation. Export data can reveal shipment frequency, but it may not fully show factory capability. That is an important weakness. Rankings should be reviewed against current audit results, samples, and recent delivery records.

Tips: Ask for production capacity by month, not vague annual figures. Check thread gauges, tensile-test reports, coating thickness, and material certificates. Compare rejected samples with approved samples. Confirm whether heat treatment is performed in-house. A factory may look efficient on paper, yet poor packaging can damage threads during a long sea journey. Suppliers should also explain corrective actions when a batch fails inspection. Perfect records are uncommon; transparent responses are more valuable.

Strength Classes 8.8–12.9: Tensile, Yield, and Hardness Requirements

When evaluating China’s top double-end bolt manufacturers, strength-class evidence matters more than polished catalogs. ISO 898-1:2013 assigns Class 8.8 a minimum tensile strength of 800 MPa and yield strength of 640 MPa. Class 10.9 reaches 1,040 MPa tensile strength and 940 MPa yield strength. Class 12.9 requires 1,220 MPa tensile strength and 1,100 MPa yield strength. These figures describe the steel, not the complete assembly.

Hardness offers a useful cross-check. ISO 898-1 lists approximate Vickers ranges of 250–320 HV for 8.8, 320–380 HV for 10.9, and 385–435 HV for 12.9. ASTM F606/F606M test procedures support tensile and hardness verification on finished fasteners. A reliable manufacturer should provide heat-treatment records, lot traceability, and independent test certificates. Ask for proof-load results too.

Threaded ends can distort test results. Testing a finished double-end bolt is better than testing only raw bar stock. Surface decarburization is another practical concern. It may reduce thread strength while hardness readings still appear acceptable. This is easy to miss. In my experience, supplier comparisons fail when buyers check only tensile strength. Dimensional accuracy, thread fit, hardness mapping, and fracture location deserve equal attention. A certificate helps, but it does not replace sample inspection.

M6–M100 Size Coverage, Thread Accuracy, Materials, and Surface Coatings

China’s top 10 double end bolt manufacturers should be assessed by more than production volume. The critical question is size coverage, from compact M6 fasteners to heavy M100 designs. Experienced factories usually show inspection records for each diameter range. They also explain how cold forming, turning, or hot forging affects the final bolt.

Thread accuracy matters during installation. For M6 parts, a small pitch error can cause cross-threading. For M100 bolts, poor alignment may create uneven load distribution.

Reliable manufacturers inspect thread pitch, major diameter, flank condition, and gauge results. ISO metric thread references can support this process, but certificates alone are not enough.

Ask for sample measurements. Ask for actual reports.

Material selection should match load, temperature, and corrosion exposure. Common choices include carbon steel, alloy steel, and stainless steel. Heat treatment records should identify hardness and process controls. Surface coatings may include zinc plating, hot-dip galvanizing, black oxide, or specialized anti-corrosion finishes. Coating thickness must not damage thread fit.

This detail is often overlooked. A bright surface proves little. Salt-spray hours also need careful interpretation, because testing rarely matches every outdoor environment. In practice, buyers should compare drawings, samples, batch traceability, and packaging protection. Even strong suppliers can miss a detail. That is why final inspection remains necessary.

ISO 9001, IATF 16949, ASTM, and Full Traceability for Global Buyers

China Top 10 Double End Bolt Manufacturers?

For global buyers, a top-ten list should begin with evidence, not factory photographs. ISO’s 2023 Survey recorded more than 1.2 million ISO 9001 certificates worldwide, showing how common quality registration has become. Yet certification alone does not prove consistent double end bolt performance. Buyers should verify certificate scope, audit dates, calibration records, and corrective-action history.

IATF 16949 matters when studs enter automotive assemblies. It requires risk-based controls, process monitoring, supplier management, and documented problem resolution. ASTM requirements then help define material, dimensions, thread quality, mechanical strength, and testing methods.

A qualified manufacturer should provide heat numbers, mill certificates, batch records, coating details, and final inspection reports. Full traceability should connect one carton to one production lot. Small details matter.

During factory evaluations, inspect thread gauges beside the production line. Check whether operators record actual readings, rather than copying target values. That weakness still appears in real audits. A useful supplier can explain why a lot was rejected and how recurrence was prevented.

ISO 9001 and IATF 16949 certificates should be confirmed through accredited certification databases, not only emailed PDFs. ASTM publishes more than 12,000 standards, so buyers must identify the exact applicable specification before comparing quotations. Cost should be reviewed after evidence. Not before.